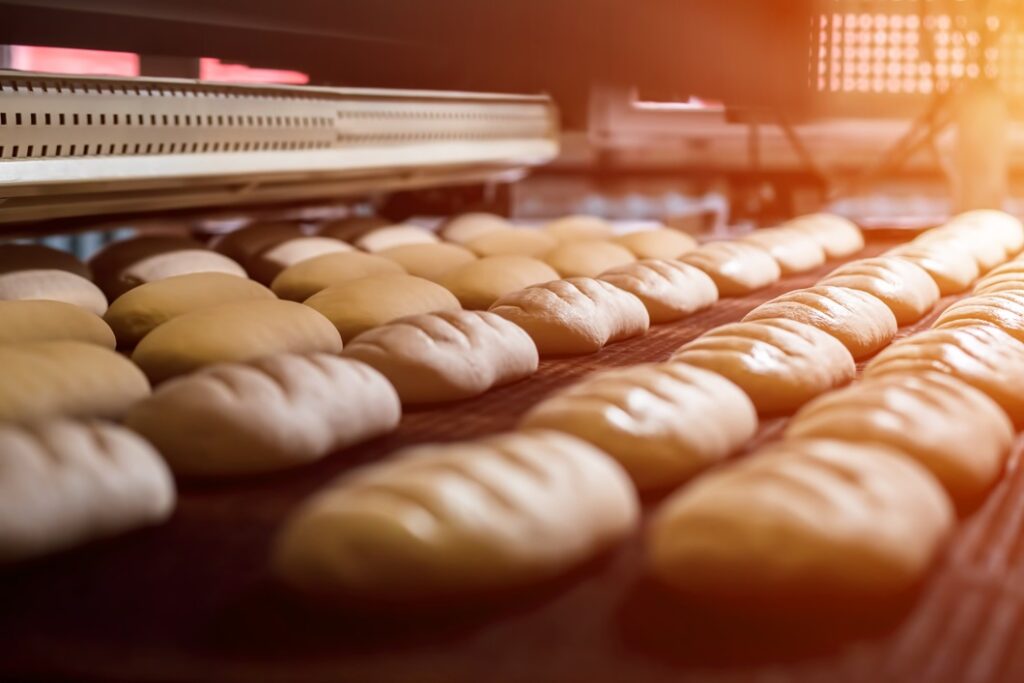
Choosing the right conveyor system can have a major impact on the efficiency, safety, and productivity of your production line. Whether you are moving components through manufacturing, transporting finished goods, or improving material handling across your facility, the system you choose should be matched carefully to your operation.
Two widely used options are floor conveyors and overhead conveyors. Both can be highly effective, but they suit different environments and handling requirements.
At KP Conveyor Services Ltd, we have over 30 years’ experience designing, manufacturing, and installing material handling systems. In this guide, we explain the key differences between floor and overhead conveyors, their advantages, and how to decide which solution is right for your business.
What Are Floor Conveyors?
Floor conveyors are installed at ground level and are commonly used to move products, parts, pallets, containers or materials through a production, assembly, storage, or dispatch area.
They can include belt conveyors, roller conveyors, chain conveyors, slat conveyors, and pallet conveyors. The best option depends on the size, weight and shape of the items being transported, as well as the speed and layout of your process.
Floor conveyors are often used in manufacturing plants, warehouses, distribution centres, packaging lines, assembly areas, and general material handling environments. Because they are positioned at floor level, they are easy to access, maintain and integrate with existing machinery.
They are a practical choice for businesses wanting a clear, reliable route for materials through a production or warehouse space.
What Are Overhead Conveyors?
Overhead conveyors are installed above the working area, using ceiling-mounted or elevated track systems to transport items through a facility. Products are usually suspended from carriers, hooks, hangers, or fixtures and moved along a defined route.
By using the space above the production floor, overhead conveyors can free up valuable ground space and improve workflow in busy facilities. They are often used where products need to be moved between workstations without obstructing operators, vehicles, or floor-based equipment.
Overhead conveyors are commonly used in paint lines, finishing processes, automotive manufacturing, component handling, assembly operations and storage or buffering systems.
For many businesses, overhead conveyors offer an efficient way to make better use of available space while keeping products moving smoothly through the production process.
Space and Layout Considerations
One of the biggest differences between floor conveyors and overhead conveyors is how they use space.
Floor conveyors require dedicated floor area. This can work well where there is enough room and where the conveyor can be incorporated into the natural flow of the facility. However, in busy environments, a floor conveyor may reduce available working space or affect access routes.
Overhead conveyors make use of vertical space. This can be particularly useful in factories or warehouses where the floor is already occupied by machinery, operators, storage zones, or forklift routes. By moving materials overhead, businesses can often improve movement through the facility without increasing the production line’s footprint.
If your site has unused overhead space and a congested floor layout, an overhead conveyor may be a suitable option. If your products are better suited to stable, floor-level transport, a floor conveyor may be the better choice.
Product Type and Handling Requirements
The type of product being moved is another crucial factor.
Floor conveyors are well suited to items that can sit securely on a belt, roller, pallet, or chain system. This includes boxes, cartons, totes, pallets, trays, packaged goods, and heavy components. They can be designed to manage a wide range of loads, including bulky or irregular items.
Overhead conveyors are better suited to items that can be suspended, hung, or carried using a dedicated fixture. This makes them useful for parts that need to be accessed from multiple sides, coated, dried, assembled or moved through a process without touching a floor-level surface.
For example, overhead conveyors are often used where components need to pass through a spray booth, curing area or finishing line. They can allow operators or automated equipment to access the product more easily while maintaining consistent movement through the process.
When choosing between floor and overhead conveyors, consider the size, weight, shape, stability, and fragility of the items being managed.
Workflow and Production Efficiency
Both floor and overhead conveyors can improve efficiency, but they do so in different ways.
Floor conveyors can create a clear and consistent path for products through a process. They are effective for linear production lines, packing areas and warehouse operations where goods need to move from one stage to the next in a controlled way.
Overhead conveyors can support more complex workflows. Because they can travel above work areas, around obstacles and between different zones, they can help create efficient routes through facilities where floor space is limited or where the process involves multiple stages.
A well-designed conveyor system can reduce manual handling, improve consistency, minimise delays and create a smoother production flow. However, the system must be designed around the specific requirements of the site.
At KP Conveyor Services Ltd, we take the time to understand your production process before recommending a solution. This allows us to design and install a system that supports your workflow, rather than forcing your operation to adapt to the conveyor.
Safety and Accessibility
Safety should always be central to conveyor system design.
Floor conveyors are easy to access for loading, unloading, maintenance, and inspection. However, because they are installed at floor level, they must be carefully positioned to avoid creating trip hazards, access restrictions or conflicts with pedestrian and vehicle routes.
Overhead conveyors can reduce obstruction at floor level, helping to keep walkways and working areas clearer. However, they require careful planning to ensure safe installation, suitable load support, appropriate guarding, and safe access for maintenance.
The right choice depends on your site layout, workforce movement, loading requirements, and maintenance procedures. In many cases, safety can be improved through a bespoke conveyor design that considers how people, products and equipment move through the space.
Installation and Integration
Installation requirements can vary between floor and overhead conveyor systems.
Floor conveyors may be easier to install in some environments because they are positioned on the floor and can often be added to existing production areas with less structural work. They may also be easier to modify or extend depending on the system design.
Overhead conveyors usually require more detailed planning. The building must be suitable to support the system, or a separate support structure may be needed. Routes also need to be planned around lighting, ventilation, doors, machinery, and other overhead services.
That said, overhead conveyors can be an excellent long-term investment when designed correctly. They can transform how a facility uses space and can be integrated into automated or semi-automated production processes.
At KP Conveyor Services Ltd, we design, manufacture, and install conveyor systems tailored to each client’s operational requirements, ensuring both practical performance and long-term reliability.
When Is a Floor Conveyor the Best Choice?
A floor conveyor may be the best option if your products are boxed, packaged, palletised or stable. It is also a strong choice if you have sufficient floor space, need easy access for loading and unloading, or your process follows a straightforward production route.
Floor conveyors are often suitable for heavy or bulky items and can integrate well with existing floor-level equipment. They are versatile, reliable and practical for many material handling tasks.
For businesses looking to improve movement through a production, warehouse or assembly environment, floor conveyors can provide a dependable and efficient solution.
When Is an Overhead Conveyor the Best Choice?
An overhead conveyor may be more suitable if floor space is limited or if you want to keep walkways and work areas clear. It is also a good option where products can be suspended or carried overhead, or where items need to pass through finishing, coating, or drying processes.
Overhead conveyors can also be useful when products need to move between several workstations or when the route must avoid floor-level obstacles. They are particularly effective in manufacturing environments where space, process flow and continuous movement are critical.
Can Floor and Overhead Conveyors Work Together?
In some facilities, the most effective solution may involve both floor and overhead conveyors.
For example, a floor conveyor might be used to transport packaged goods through a dispatch area, while an overhead conveyor moves components through production or finishing. By combining systems, businesses can create a complete material handling solution that supports different stages of operation.
A bespoke approach allows each area of the production line to use the most suitable conveyor type, helping improve efficiency, reduce manual handling, and create a safer, more organised working environment.
Speak to KP Conveyor Services Ltd
There is no one-size-fits-all answer when choosing between floor conveyors and overhead conveyors. The right solution depends on your products, available space, production goals, safety requirements, budget, and future plans.
At KP Conveyor Services Ltd, we specialise in the design, manufacture, and installation of conveyor systems for material handling applications. With over 30 years of experience, we understand how important it is to choose the right system for your production line.
Whether you are considering a new floor conveyor, an overhead conveyor, or a complete bespoke conveyor system, our team can help you find the right solution.
To discuss your requirements, contact KP Conveyor Services Ltd today.
Recent Posts
-
 Floor Conveyors vs Overhead Conveyors: Which Is Right for You?
-
 How Conveyor Systems Improve Efficiency and Reduce Costs in UK Manufacturing
-
 Boost Your Production Line: The Ultimate Guide to Maximising Efficiency with Conveyor Systems
-
 The Future of Material Handling and Breakthroughs in Conveyor Technology
-
 A Guide to Choosing the Perfect Conveyor System for Your Industry